Remote site grout plant: containerized buying notes
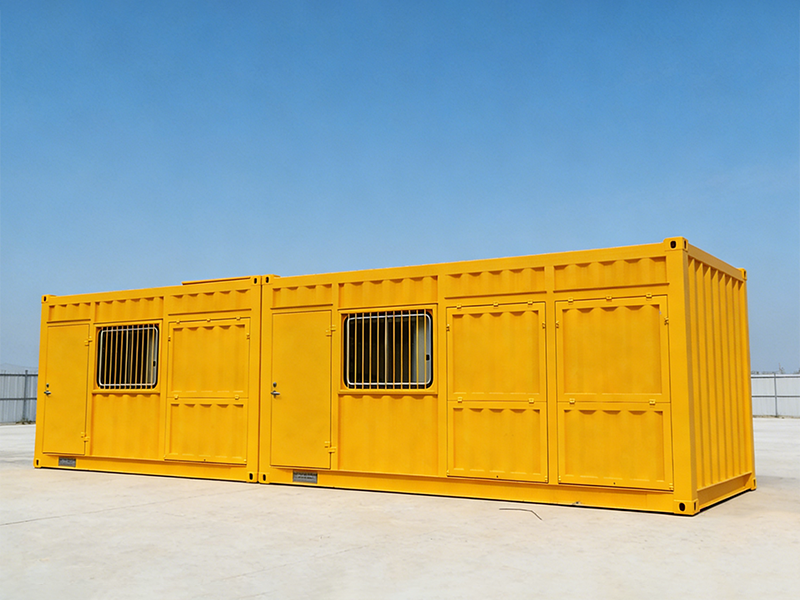
Here is the plain version: containerized grout plant for remote sites should be specified from the job site backward. The plant has to fit the transport route, the cement supply plan, the output target, the control requirement, and the people who will clean and operate it after a long shift.
Procurement memo for the first RFQ
Put the site constraint at the top of the inquiry. If the project is remote, indoor, marine, height-restricted, or short on lifting equipment, say that first. the works can then judge whether AGP-I is the right starting point or whether another layout should be discussed. For the feed and storage side, see the article on product.
The next line should cover containerized automated grout plant and 30-40 m3/h containerized grout plant planning. A buyer who only asks for a model number usually receives a broad answer. A buyer who gives output, recipe, cement supply, power, and record needs gets a more useful discussion.
Good RFQs are not longer because they are formal. They are longer because they remove avoidable assumptions.
The details that prevent rework
Confirm the downstream equipment before the plant is priced. The pump, hose, injection rig, soil mixing equipment, or DCM spread has its own rhythm. If the plant cannot supply that rhythm, the site waits. If the plant is oversized, the buyer pays for capacity that may not be used.
For AGP-I, review 20 ft grout plant, 40 ft grout plant, and all-weather containerized grout plant before price comparison. Those items affect the layout, control cabinet, feeding package, and commissioning plan.
Quotation checks
| Point to confirm | What to send | Why it changes the quotation |
|---|---|---|
| Work method | remote grouting, indoor tunneling, emergency reinforcement, and fast deployment | The grout plant should follow the construction method, not a generic catalogue label. |
| Production rhythm | 30-40 m3/h containerized grout plant planning | A plant that is too small creates waiting time; a plant that is too large can add cost and cleaning work. |
| Material feeding | Cement, lime, dry powder, bulk silo, screw conveyor, or bag feeding | Feeding method changes footprint, labor, dust control, and daily reliability. |
| Control requirement | Recipe, water-cement ratio, admixture channels, pressure, flow, and batch records | These details affect PLC configuration and site documentation. |
| Site limit | Height, width, access road, indoor work, marine exposure, wind, or remote power | Layout restrictions often decide the model before output does. |
Questions Eizoo should be able to answer
Ask how AGP-I handles material feeding, operator control, cleaning, and records under the stated site condition. Ask what information is still missing. A careful supplier should point out the unknowns before presenting the final configuration. For the configuration used on larger sites, see the SC/G Series for metered feed.
Also ask which connected equipment should be reviewed together. For many jobs, silo capacity, screw conveyor route, mixer duty cycle, pump interface, and data output are part of the same decision.
Frequently asked questions
What should I confirm before asking for AGP-I pricing?
Send the work method, hourly output target, material supply method, mix or binder requirement, site restrictions, power supply, downstream equipment, and record format. Eizoo can then review the plant as a working system rather than a single machine. Buyers who ask about remote site grout plant usually raise it with a China grout plant manufacturer first, because the tolerance data settles most of the argument.
How do I know whether containerized grout plant for remote sites fits my project?
Start with the field method and the bottleneck. If output is the bottleneck, check production capacity and mixer duty cycle. If access is the bottleneck, check footprint, height, transport, and feeding route first.
Why do records matter in grout plant selection?
Pressure, flow, W/C ratio, recipe, and batch records help the site team compare planned production with actual production. They also make shift handover and client review easier.
Should I choose bag feeding, silo feeding, or screw conveyor feeding?
Small intermittent jobs may tolerate bag feeding. Longer shifts normally need a cleaner cement or powder supply path, often with silo storage and screw conveyor feeding matched to mixer demand.
What makes a quotation faster and more accurate?
Photos, layout drawings, target output, recipe details, cement consumption, site limits, power information, and QA/QC requirements remove most guesswork before the first proposal.
Before you send the inquiry
Send Eizoo the project method, target output, cement or powder supply method, water and admixture requirements, site restrictions, power supply, downstream equipment, cleaning expectations, and record format. With those details, the first reply can focus on the right layout instead of asking for the basics again.
For remote-site project teams, a good plant discussion should stay close to the work. Output matters, but so do the parts of the day that are easy to forget: cement delivery, shift changes, line flushing, sensor checks, and where operators stand when the site is busy. For the equipment side of the same problem, see the HS-Series storage silos for grout plants.
The same logic applies to containerized grout plant with pressure printout. The term is useful only when it points to a specific requirement in the field, such as dosing accuracy, feeding continuity, lower height, easier transport, or a printout that the client can review.
If two quotations look similar, compare the assumptions. One may include silo integration, record output, dust collection, and commissioning support, while the other may leave those items open. The cheaper number is not always the lower-risk package.
This is also where buyer questions help conversion. A contractor who can describe soil condition, grout ratio, daily cement use, access limits, and reporting needs is already close to a serious equipment conversation. Buyers who ask about remote site grout plant usually raise it with a China grout plant manufacturer first, because the tolerance data settles most of the argument.
A second look should focus on remote grouting, indoor tunneling, emergency reinforcement, and fast deployment rather than on the product name alone. The real test is whether the plant can keep the material path steady from storage to discharge and still leave the crew enough room to work cleanly at the end of the shift.
For remote-site project teams, the important question is whether the quotation matches the job rhythm. A plant that fits the output target but creates extra waiting time, extra cleaning, or extra handoff work is usually the wrong answer in practice.
The linked equipment should be reviewed as one line. AGP-I containerized grout plant, SC/G Series digital screw conveyors, and the rest of the feeding chain affect the same job, so it makes more sense to compare them together than to price each item in isolation.
When the buyer asks about 20 ft grout plant, the hidden question is usually about layout, access, and control. If that part is unclear, the first proposal will spend too much time guessing instead of solving the site problem.
The safest RFQ is the one that names the site limit, the output rhythm, and the record requirement in plain English. That gives Eizoo a better base for matching containerized grout plant for remote sites with the rest of the production chain. Sites comparing remote site grout plant ask a grout plant supplier in China for the tolerance data first.
A final check is simple: can the crew clean it, inspect it, and keep it honest after the first busy week? If the answer is not obvious, the configuration still needs work. Open the write-up on AGP-I containerized grout plant for indoor for the record format used on site.
Start with the site drawing before comparing models. Mark the cement source, water point, plant position, discharge route, cleaning area, and the downstream rig or pump. That simple drawing usually shows whether containerized automated grout plant is mainly an output question, a footprint question, or a material-handling question.
Hourly output should be checked against the real work cycle, not just a catalog range. Some sites need a steady supply for long shifts, while others need shorter runs with frequent cleaning. 30-40 m3/h containerized grout plant planning only has value when it matches the downstream demand and the crew can keep the line ready.
Material supply is often the quiet bottleneck. A plant can have the right mixer and still lose time if cement delivery, silo discharge, or conveyor feeding is not stable. When buyers discuss 20 ft grout plant, they should also explain how material arrives on site and the conveying distance it must cover. Supervisors usually ask for remote site grout plant checklist when the numbers stop matching the recipe.
Water and admixture planning deserve the same attention as cement. If the project changes grout ratio, uses several admixtures, or works through different soil conditions, the control package has to make those changes clear to the operator. Good control is practical, not decorative.
Record needs should be named early. Pressure, flow, W/C ratio, batch number, recipe name, and printout format can all affect instruments and control logic. Waiting until the plant is nearly specified makes the quotation less stable and creates avoidable revisions.
Cleaning access is not a small detail in cement slurry work. Valves, mixer areas, hoses, covers, and discharge points need room for routine washing and inspection. If the layout saves space but makes cleaning hard, the crew will pay for that decision every day. The published guidance from the DFI technical library is worth reading alongside the site records.
For remote-site project teams, maintenance planning should include spare parts, wear points, sensor checks, and the easiest way to clear blocked material. A supplier should be able to explain the parts of the system most likely to need attention during a demanding project. For the tolerance data behind these checks, see the field notes on AGP-I containerized grout plant vs fixed-site. Crews tend to look for remote site grout plant causes before they touch the hardware.
Transport and lifting limits can decide the configuration before output does. Buyers should share road width, crane access, container limits, low bridges, indoor doors, platform limits, and any rule that affects installation. Those details keep containerized grout plant for remote sites tied to a real working envelope.
The connected equipment matters because a grout plant rarely works alone. Storage, screw conveyor, mixer, agitator, pump, hose, and field rig all have their own pace. A strong proposal explains how those pieces stay synchronized instead of treating each component as a separate purchase.
If the job involves remote grouting, indoor tunneling, emergency reinforcement, and fast deployment, the buyer should describe the construction sequence. Continuous work, intermittent injection, dry powder addition, marine placement, and compact urban operation all ask different things from the same general plant family.
Noise, dust, splash, and operator position are easy to overlook during early comparison. They become very visible once the plant is running near traffic, existing structures, or other trades. A practical layout gives operators clear access without forcing them into unsafe shortcuts.
Commissioning questions should be included in the first inquiry. Ask what information Eizoo needs before delivery, which checks happen during startup, and what site utilities must be ready. That prevents the first week from turning into a search for missing basics. New operators are given remote site grout plant field notes in the first week.
The best buyer notes are often photos, not long descriptions. A few pictures of access roads, working space, cement storage, water supply, and nearby obstacles can remove confusion that a written RFQ leaves open.
For quotation comparison, separate what is included from what is assumed. One offer may include feeding equipment, record output, dust handling, and commissioning support, while another may leave those items outside the main number. The difference matters more than a neat price table.
Operators also need a simple way to see whether the plant is behaving normally. Alarms, recipe names, flow changes, and feed interruptions should be visible enough that the crew can react before the downstream process waits too long. For the layout side of the same problem, see the AGP-V60 heavy-duty grout plant.
A buyer planning several projects should ask whether the chosen setup can handle nearby applications without becoming oversized for the current job. Flexibility is useful only when it fits real methods, real materials, and real site restrictions.
If the plant will work in remote, marine, indoor, or low-clearance conditions, say that in the first message. These conditions change access, corrosion exposure, ventilation, storage, power, and cleaning more than many buyers expect. For projects working to a stated specification, the site file usually has to show EN 12715 grouting records.
A useful final inquiry does not need sales language. It needs target output, material details, site limits, downstream equipment, record needs, and photos. With those facts, Eizoo can respond with a configuration that feels like it belongs on the site.
Ask what happens on the worst normal day, not the best demonstration day. If cement arrives late, powder flow changes, water pressure drops, or the crew has to clean under time pressure, the plant still needs a workflow that people can follow without inventing shortcuts.
The buyer should also describe how often the mix or binder condition changes. A job that repeats one recipe all day has different control needs from a job that switches between several grout ratios, admixture combinations, or treatment stages.
For 40 ft grout plant, the quotation should explain the practical boundary of the system. That boundary may include the storage package, feeding device, control panel, mixer, discharge connection, and the record output expected by the client.
Some buyers compare only motor power or output. A better comparison includes the people around the plant: who loads cement, who watches the screen, who handles wash-down, who reads the record, and who signs off the shift report.
If the site uses bulk material, the refill plan should be checked before layout approval. Cement truck position, silo capacity, conveyor angle, venting, dust collection, and safe walking space all affect whether the plant can run without constant interruption.
If the site uses bags, labor and dust become part of the production calculation. Bag handling may be acceptable on short jobs, but the buyer should be honest about daily consumption, crew size, weather exposure, and how material is protected before mixing. For the commissioning view of the same plant, see the automated grout plant systems.
For all-weather containerized grout plant, the project team should ask how the system behaves during start, pause, restart, and cleaning. Many issues do not appear during steady operation; they appear when the site has to stop and recover quickly.
The maintenance conversation should include ordinary tools and ordinary access. A plant that needs difficult access for simple inspection points will be harder to keep reliable, especially when the work area is muddy, crowded, or shared with other equipment.
Documentation is also a buyer concern. If the owner expects production records, the plant should make those records easy to collect and understand. A record that operators avoid using will not help much during dispute review or handover.
When comparing containerized grout plant with pressure printout with another configuration, ask which risk each option removes. One layout may reduce height risk. Another may reduce transport work. Another may make cleaning easier. The right answer depends on which risk is most expensive on that job.
Site teams should avoid hiding uncertainty. If the mix design is not final, if soil conditions may change, or if the downstream equipment is still being selected, say so. Eizoo Machinery can still discuss a sensible range, but the quotation should not pretend those choices are already fixed.
The most useful inquiry usually fits on one clear page with photos attached. It names the method, output, material route, control needs, site limits, and contact person. That is enough to start a serious technical conversation without burying the supplier in vague wording.
Before ordering, ask what the operator sees during a normal shift. The screen, alarms, manual controls, record buttons, and cleaning steps should make sense to the person standing beside the equipment, not only to the person reading the proposal.
A good plant choice should make the site calmer. It should reduce waiting, reduce guesswork, keep material moving, and give the buyer clearer information before money is spent on mobilization, accessories, or late changes.
If the project has a strict working window, the buyer should mention it early. Night work, traffic closures, tide windows, or short access permits can make cleaning speed and startup reliability more important than a small difference in rated capacity.
Sending the batch log, the calibration sheet, and the material certificates to the manufacturer’s service team is what turns a symptom into a component list. Eizoo keeps the weighing and metering documentation with the plant, so the next enquiry starts from records rather than from memory.